Skip to content
Back

Six steps from copper to a labelled reel

We draw the copper, extrude the insulation and jacket, lay up the pairs and test every construction ourselves: the six steps below are the sequence each cable on this site goes through. Production runs in Guangdong, China — the plant address and line list are given to customers who ask, because a plant visit says more than a page of numbers.

68part numbers
5cable families
6production steps
9standards referenced

Ask a technical question WhatsApp

1 2 3 4 5
  1. 1 JacketPVC · LSZH · PE
  2. 2 Braidaluminium-magnesium wire
  3. 3 Foilaluminium, bonded to drain wire
  4. 4 Cross fillerholds the four pairs in place
  5. 5 Pairtwisted, HDPE insulation, copper core
Shielded construction, layer by layer — the layers in the order the process below builds them.

Scope at a glance

Production siteGuangdong, China — plant address provided to customers on request
OfficeRoom 305X, Huilange Building, No. 273 Huangpu Boulevard West, Tianhe District, Guangzhou, Guangdong, 510620, China
Product familiesNetwork Cables · Multi-Pair & CCTV Cables · Patch Cords · HDMI & Display Cables · Power Cords
ConstructionsUTP, FTP, SFTP, SSTP network cable · multi-pair from 2 to 50 pairs · SYV coaxial · RVV / RVVP control · patch cords CAT5E to CAT8 · HDMI, DisplayPort, fibre HDMI · moulded power cords
Jacket optionsPVC · LSZH · PE (outdoor, with water block)
Standards referencedUL758, UL1581, UL444, TIA/EIA-568, CSA C22.2, ISO/IEC 11801, YD/T1019-2001, GY/T135-1998, SJ/T11138-1997
Business modelOEM and ODM for distributors, system integrators and brand owners
CustomisationJacket colour and print, part numbering, reel or box length, carton and pallet marking

Capacity, headcount and line count are given in the quotation, because all three move with the season and a static number on a website is only ever wrong by the time it is read.

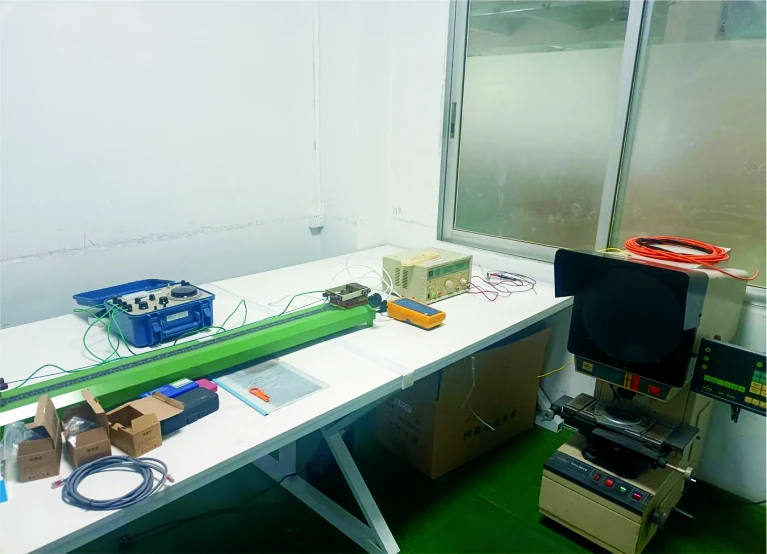
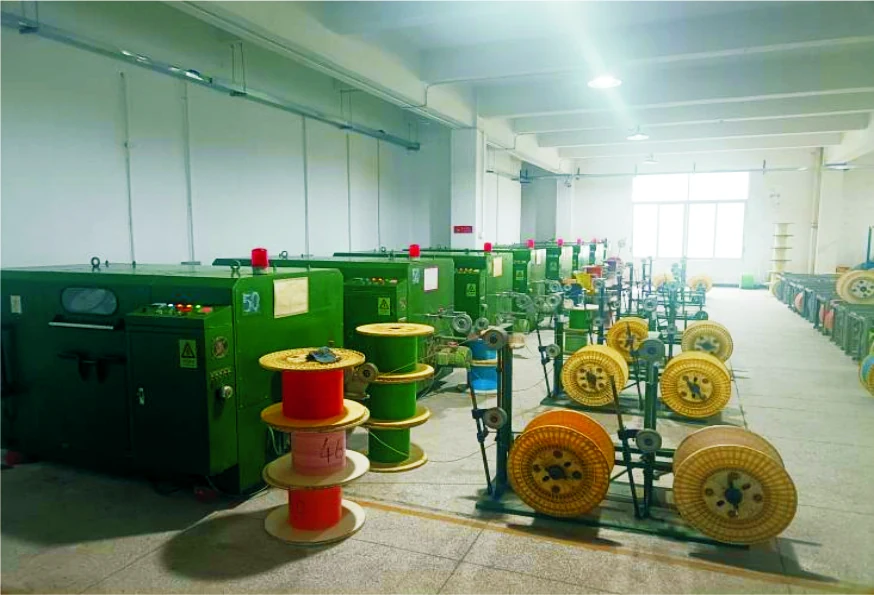
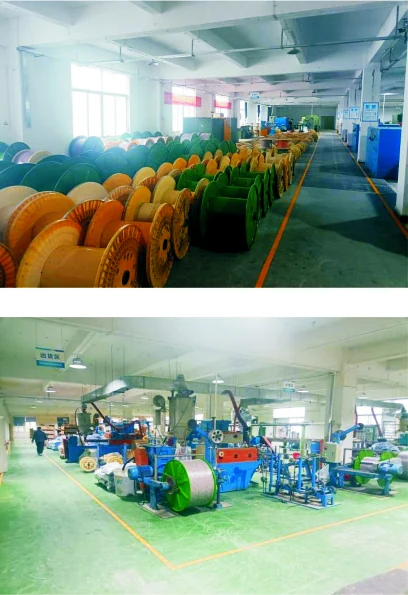
On the floor

Photographs from the production site: the extruding and cabling lines, finished reels before packing, and the test bench each construction is checked on.

Extruding and cabling lines in the production hall, with cable reels between the machines
Extruding and cabling lines — insulation and jacket are extruded in-house.
Finished cable reels stacked before packing
Finished reels before packing, labelled to the customer's part number.
Test bench with instruments for electrical testing of cable samples
Test bench: conductor resistance, insulation resistance, capacitance and continuity.

Site photographs are on request as high-resolution files, together with the line list — see how to ask.

The six production steps, in order

Each step maps to a layer in the cutaway above — conductor, insulation, pair lay-up, shield, jacket. Scroll through the line, left to right.

01

Conductor drawing

Bare copper rod is drawn to the finished conductor diameter — 0.40 mm to 0.58 mm depending on the family — and annealed so the conductor stays soft enough to lay up without cracking. Every cable on this site starts as bare copper; our specification calls it out explicitly for all network, multi-pair and control constructions.

02

Insulation extrusion

HDPE is extruded over the conductor to a controlled wall: 0.9 mm on CAT5E and CAT6 pairs, 1.0 mm on the double shielded CAT5E, 0.9–1.36 mm on the multi-pair range. Insulation concentricity is what holds the impedance at 100 ± 15 ohm later in the test.

03

Pairing and lay-up

Pairs are twisted at their designed lay lengths and cables from 5 to 200 pairs are laid up in layers. On CAT6 and above a PE cross filler is added to keep the four pairs in a fixed geometry — visible in the cutaway on the factory page.

04

Shielding

FTP constructions take aluminium foil with a drain wire; SFTP and SSTP constructions add an Al-Mg alloy braid over the foil. On the coaxial range the shield is aluminium foil plus tinned copper braid at 64, 96 or 128 strands, which is the number printed in the part number.

05

Jacket extrusion

The jacket is extruded in flame-retardant PVC, low smoke zero halogen compound, or PE for outdoor constructions. Outdoor cable adds waterproof paper and an inner sheath before the outer PE jacket. Colour and surface printing are set by the customer's part-number convention.

06

Electrical test and packing

Finished cable is checked against the limits published on this site: conductor resistance, insulation resistance, mutual capacitance, characteristic impedance and, on the data cables, transmission performance. Reels and boxes are labelled to the customer's as-built documentation before packing.

What is tested, and to what limit

These are the same values printed on the product pages, so they can go straight into a purchase order as the acceptance criteria.

PropertyLimitApplies to
Characteristic impedance100 ± 15 ohmCAT5E network cable
Max. conductor resistance<= 9.38 ohm / 100 m at 20 °CCAT5E network cable, patch cords
Insulation resistance>= 5000 Mohm.kmNetwork, multi-pair, patch cords
Mutual capacitance<= 5.6 nF / 100 m (network), <= 6.6 nF / 100 m (multi-pair)Network, multi-pair
Capacitance unbalance pair-to-earth<= 330 pF / 100 mMulti-pair cable
DC resistance unbalance<= 3 %Multi-pair cable
Operating / installation temperature-20 to 75 °C (network), 0 to 60 °C (multi-pair installation)Network, multi-pair
Coaxial impedance75 ohmSYV-75-3, SYV-75-5
Standards the constructions are tested against
  • UL758
  • UL1581
  • UL444
  • TIA/EIA-568
  • CSA C22.2
  • ISO/IEC 11801
  • YD/T1019-2001
  • GY/T135-1998
  • SJ/T11138-1997

Test reports and certificates

Reports are issued against the exact part number quoted — construction, jacket and part-number print — so the document matches the goods on the pallet. Tell us which markets the goods are going to and we return the report set that applies there (UL and CSA references, TIA/EIA-568, ISO/IEC 11801, and the Chinese standards listed above).

How an OEM order runs

1. Specification review

You send the part-number list or the specification: category, shield, jacket, colour, printing, packing. If a value is not in our range we say so and quote against your drawing instead of substituting.

2. Quotation

We return price, MOQ, lead time and packing per line item. Commercial terms are confirmed in writing; nothing about price or lead time is published on this site because both depend on the mix and the shipping term.

3. Sample

For OEM items the jacket print, colour and packing artwork are confirmed on a sample before production. Sample lead time and cost are part of the quotation.

4. Production and in-process test

Cable is run against the limits in the QC table, then reeled or boxed and labelled to the customer's numbering so the goods can go into your warehouse without relabelling.

5. Pre-shipment check and loading

Reel and carton count, label check and packing photos before loading. Inspection by a third party is welcome at your arrangement.

What we deliberately do not publish

Test reports and certificates: supplied per part number on request, as the issuing lab's document for that construction — not as a generic company PDF. We do not retype certificate numbers from a picture.
Production capacity, headcount and line count are quoted when you ask: they change with the season, so the figure we give is the one that applies to your run.
Prices, MOQ and lead times are quoted per order: they follow the part-number mix, the quantity and the shipping term, and the line is set up for that mix.
Where the specification leaves a field blank (patch cord length, HDMI version, plug certification), the value is set on the line for your order — the product page says which fields those are.
Ask for what is missing See the range

WhatsApp Email